
Key Takeaways
- A works test proves a unit, not the assembly you end up with.
- Site work adds joints, and every new joint is a new thing to prove.
- Protection settings depend on your cable, so they cannot be fixed in the factory.
- Four records decide whether a fault lands on the installer or on you.
- The first week of load belongs in the contract, not in the goodwill column.
The works test proves a unit, the site proves an assembly
Ask what a routine test report covers and the answer is narrower than most buyers expect. It covers the assembly that was tested, in the condition it was tested. The standard behind that test is IEC 61439. It verifies a design and a routine test on each unit.
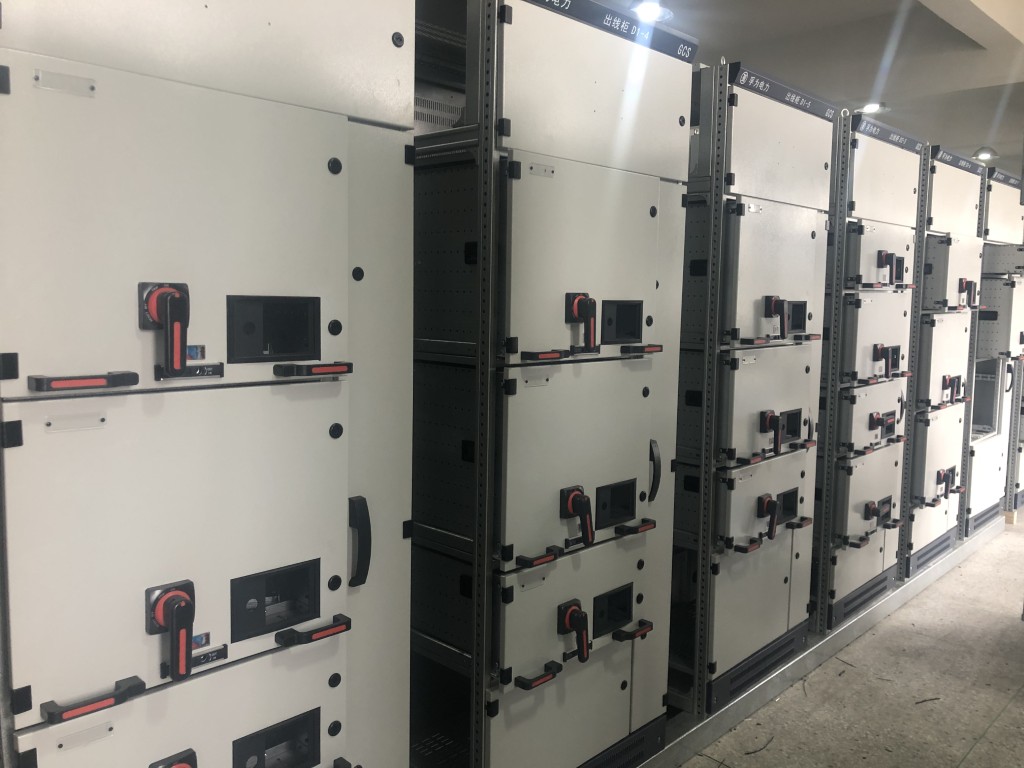
That assembly then gets split into transport sections. Joints come apart. Busbars are reconnected on your floor, and new cable arrives where the Works never planned for it.
So the object has changed. The tested article and the installed article share a design, not an identity. industrial control panels that travel in two halves carry the same gap.
This is why a folder of factory certificates proves less than it looks. Those pages describe an object that no longer exists in that form. panel builders will say the same, and their offers usually name where the scope stops.
What exists now is a new assembly, made of old parts, joined by hands that were not in the Works. It has to be proven again, and only site work can do it.
Five companies, five definitions of installation
Ask five suppliers what installation includes and you get five answers. That is not dishonesty. It is a market where one word covers everything from a delivery note to a signed energisation permit.
An industrial panel oem ships a tested assembly and stops at the gate. An electrical panel builder follows your drawing and sends a supervisor for a week. Many electrical panel companies list installation as an optional line item.
Then there is the company that lands the sections, terminates the cable and sets the relays. It hands you a signed pack. Most electrical panel builders stop at the switch room door. That last step is a different trade.
Where electrical panel fabrication happens in the works, the site crew has less to do at height. That is where the real cost difference sits, not in the labour rate.
| Scope line | Panel maker | Builder with site crew | Full-service installer |
|---|---|---|---|
| Delivery and offloading | Yes | Yes | Yes |
| Positioning, shimming, bolting down | No | Yes | Yes |
| Busbar joints torqued and logged | No | Sometimes | Yes |
| Cable termination and glands | No | Rarely | Yes |
| Protection settings and injection test | No | Rarely | Yes |
| Handover test pack | Works only | Partial | Yes |
| First week of load | No | No | Written in |
Every joint added on site is a new thing to prove
A factory busbar joint is made once, indoors, with a torque wrench on a calibration schedule. A site joint is made with dust in the air, often at height, usually at night. Someone else set that schedule.
The physics does not read the schedule. Contact resistance at a joint adds heat, and heat raises resistance again. A joint sitting 20 micro-ohms high can run 15 K hotter at full load.
Cable work carries the same risk in a different shape. A compression lug needs the correct die, and a stress cone needs a clean cut. Neither forgives a hurried afternoon.
This is the part of the job a switch gear panel leaves the works having no control over. The panel departs correct. The installation decides whether it stays correct.
That pattern repeats in mcc electrical work. The drawers leave tested, and the busbar behind them is finished on site.
 Cable compartment
Colour-coded busbars and insulators, joined on site.
Every bolted face is a new contact resistance.
Protection settings belong to the cable, not the order
A breaker setting is a promise about a cable. The promise only holds when the cable, the transformer and the device upstream are all known.
The factory knows the assembly. It does not know your feeder is 85 metres of four-core. Nor that the device upstream clears in 0.4 seconds.
So the settings get made twice. Once on paper as a study, with the fault level and the cable data. Once at the relay, with the study in hand and a tester on the leads.
Do not accept a setting sheet that arrives with the delivery. On low voltage switchgears the numbers that matter are written after the cable is pulled, not before.
Discrimination deserves its own study. Two curves that look fine on a datasheet can cross once the real cable length goes in. Nobody sees that crossing until the first downstream fault takes out the incomer.
 Breaker rows
Settings sit inside a wired assembly.
The cable that decides them arrives later.
Four records that end the argument
A handover pack is not paperwork for its own sake. It is the file that decides who pays when something fails in month four, when nobody remembers the night shift.
Record one is insulation resistance and protective conductor continuity, taken per section and per phase. Record two is the settings actually left in each relay, with the injection test that proved them.
Record three is phase sequence and interlock function, tested with the incomer open and the earth switch closed. Record four is a torque log for every joint, plus a thermal image taken under load.
Book the metal enclosures into that pack as well. Every cable entry is a sealed, recorded feature, not a hole with a gland pushed into it. The entry is inside the type test, and the record proves it was made as drawn.

A technician still has to stand at the switchgear
The first week after energisation is part of the job
Energisation is a step, not the finish line. An installation is only proven once real load has run through it for a few days.
Scan the joints at 24 hours, then again at seven days, under the heaviest load you can arrange. A joint that was tight can relax. A day-one thermal baseline is worth more than any verbal guarantee.
Load steps also show the part-load picture. The IEA puts motor-driven systems near half of global electricity use. Most of them run below full load.
Add load in steps rather than one jump. If a breaker trips in week one, the order of checks matters. Read the settings, then the event log, then the cable, and only then doubt the device.
A data centre hall makes this concrete. Two supplies, a short transfer window, and no patience for a joint that needs retightening. The monitoring layer is how week one gets watched. mcc panel suppliers will sell you that layer, but they will not read it for you.
Five risks the contract has to move
The price buys labour and material. The value sits in five risks that move from your side to theirs. Each one needs a sentence, not a schedule.
Site conditions as found. Damage between the gate and energisation. Third-party interfaces such as civil works and the utility connection. Temporary supply while the old board is still live. And the first failure inside the warranty period.
A quality system certified to ISO 9001 proves a process exists. It does not prove the crew on your floor used it.
Take the interface risk seriously. Most installers subdivide the work, and the seam between two subcontractors is where the argument starts. One name signs the handover, or nobody does.
An industrial control panel builder who subcontracts the site work is selling a product with an introduction. A supplier of industrial control panels that stops at the gate is doing the same thing. That is a fine thing to buy. The words promise something wider.
Frequently asked questions
Does a full-service installation include the incoming cable?
Can the factory set the protection relays before delivery?
How long does installing a switchgear lineup take?
What should the handover pack contain?
Who is responsible if a joint fails after handover?
Is it cheaper to buy the equipment and hire a local installer?
Do custom electrical panels change the installation scope?
Final thoughts
Full-service is a claim about the end state. The assembly leaves tested and arrives as parts. Only the site work, the records and the first loaded week turn those parts into an installation you can defend.
Send the single line diagram and the cable schedule
We will mark what belongs in the works and what must happen on your floor. Then we will list the records the handover needs.
Contact Giantele