Key takeaways
- The survey comes first. A vendor who will not list your motors in writing is quoting a box.
- The motor nameplate sets the speed range, not the drive datasheet.
- Three scopes hide under the word retrofit: door change, section change, full replacement.
- An old enclosure rarely has the depth, airflow and cable radius a drive needs.
- Ask who signs the test sheet. Fabricator and integrator carry different risk.
Most vfd panel retrofits begin with a working machine, an old motor and no drawing. A variable speed motor controller dropped into that cabinet is not a plug in swap. This guide explains how to judge the companies that quote for the job.
The short answer is that the good ones sell a survey and a report before they sell a panel. Everything below follows from that.
A retrofit is a survey before it is a purchase
The company worth hiring turns up with a clipboard, not a catalogue. The first visit is a survey of every motor the panel feeds.
That survey records the nameplate data, the cable size and the free space inside the enclosure. On a plant with thirty drives, allow two days.
Ask for the survey as a document. A vendor who will not put the motor list in writing is selling a box, not a retrofit.
Part of this work is already sold as legacy equipment panel modernization. The scope is the same: measure first, then quote.
The motor nameplate decides the drive
An old motor carries an insulation class, a duty rating and a nameplate frequency. All three change what a drive may do to it.
Class B insulation has a lower temperature limit than class F. Long cables and a high switching frequency both add heat. Set the drive to respect the older winding.
A 50 Hz motor on a 60 Hz supply needs its speed range checked before anything is ordered.
Below about 25 Hz, the shaft fan on a standard motor moves very little air. The drive must derate, or the motor needs a separate fan.
None of this appears on a drive datasheet. It appears on the motor plate, which is why the survey runs before the quotation.
Three ways to keep an old motor running
You do not have to fit a drive. Three options keep an old motor turning, and the load decides which one fits.
| Option | Starting current | Speed control | Where it fits |
|---|---|---|---|
| Direct on line | 6 to 8 times full load | None | Small pumps and fans on a strong supply |
| Star delta | 2 to 3 times full load | None | Large motors that start unloaded |
| Soft starter | 2 to 4 times, adjustable | Ramp only | Conveyors, crushers, pumps with a long start |
| VFD | 1 to 1.5 times, adjustable | Full range | Variable flow, pressure or speed |
A set of combination motor starters puts a starter and a disconnecting means in one enclosure. For a conveyor that runs at one speed, that is often the whole answer.
Choose a drive when the process varies. Choose a starter when it does not. Most plants find both answers in the same cabinet.
What vfd panel retrofits actually replace
 Door plates
A door change is not a rebuild
Three scopes are sold under one word. A door change keeps the enclosure and the busbar. A section change adds a column.
A full replacement keeps nothing but the incoming cable. Ask which one the quote describes.
A door change is a week in most works. A full replacement is a shutdown, a crane and a new cable schedule.
The incoming section is the part switchgear suppliers rarely scope in the same order. Check the short circuit rating of the old busbar before you add load to it.
Where the old enclosure runs out of room
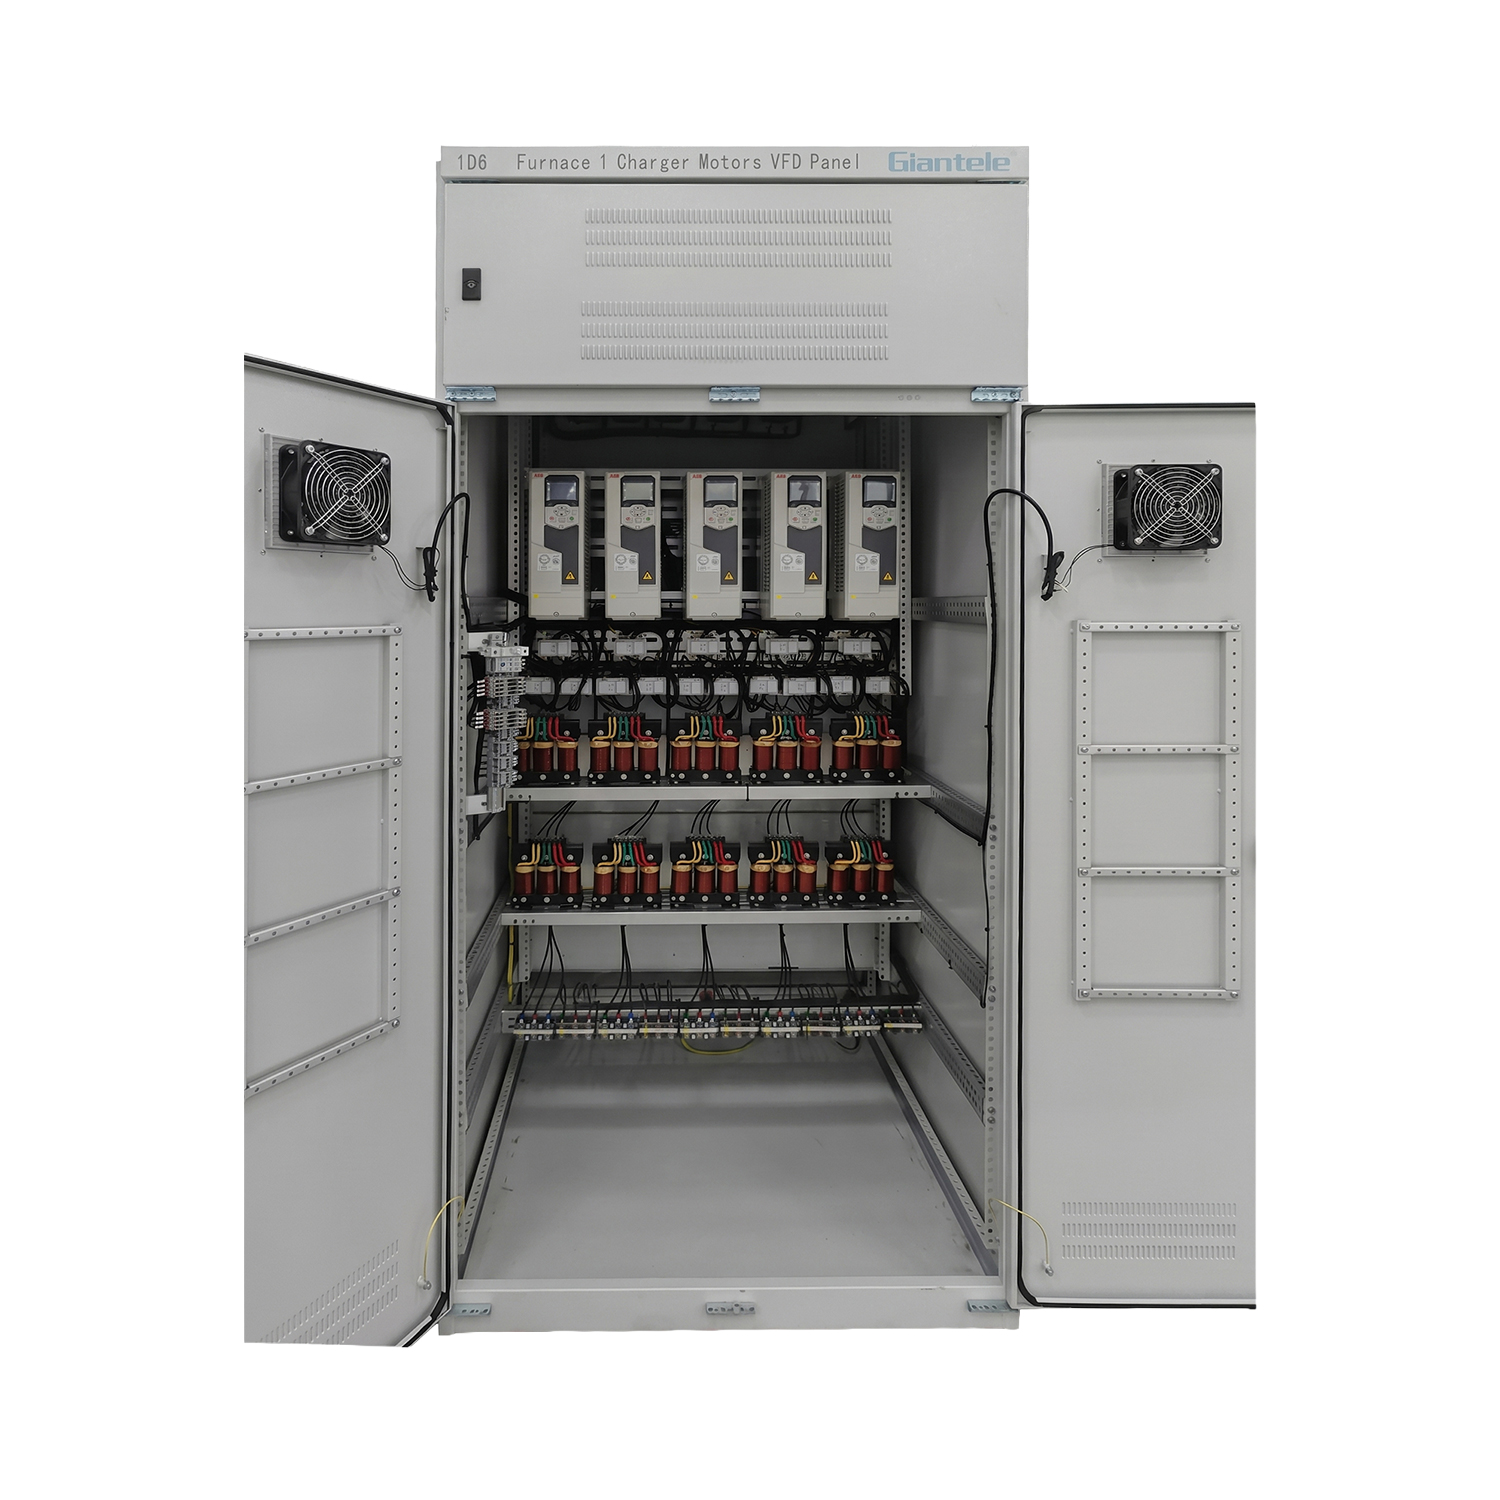
A drive needs depth, airflow and a bending radius for its output cable. An enclosure built around a contactor has none of the three.

Four things that do not fit
The output cable is the one people forget. A screened motor cable needs a gland plate to land on and room to turn.
Anything added inside that cabinet has to stay within the original IEC 61439 design verification. Cut a new hole without checking, and the assembly is no longer the one that was tested.
Local control at the door, remote control over the link
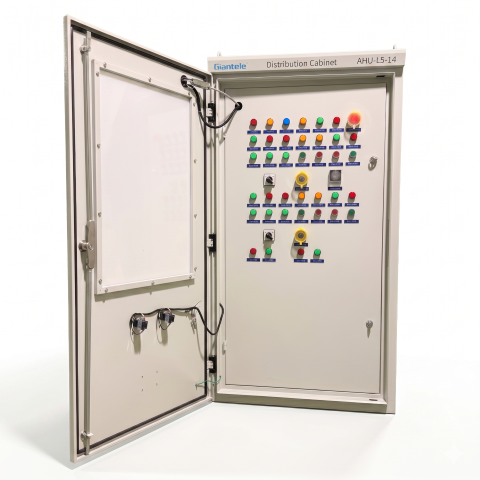
Operators want a selector, a run button and a fault lamp at the door. A vfd remote control panel is that same cabinet seen from a desk.
The hand off auto selector decides who is in charge. Wire it so the local position always wins.
Control panel control has to be settled once, in the drawing. Write the hierarchy down before commissioning, not during it.
In manufacturing control systems the order is usually PLC, then drive, then field switch. Keep that order the same in every panel you retrofit, so one training session covers the plant.
The link only repeats what the panel already holds. A vfd drive wiring diagram that names every terminal is worth more than a dashboard. The dashboard has no spare relay behind it.
When a vfd drive panel is the wrong answer
A vfd drive panel earns its price on a variable load. On a constant load it is a box of losses and a new failure mode.
Four cases where a starter beats a drive. Check your plant against them before the survey.
- A pump that runs at one duty point all day.
- A motor of unknown insulation class.
- A cable run over 100 m with no reactor fitted.
- A plant whose capacitor bank already trips.
The harmonic point matters on any site with an APFC bank. A group of drives raises the fifth and seventh harmonic, and a capacitor bank can resonate with them.
That is where electrical starters with a bypass contactor earn their keep. The motor keeps running when the drive is out of service.
Motors and the systems they drive take about 45 percent of global electricity, according to the IEA. A drive fitted where no speed change is needed is a tax on that load.
Panel fabricators, integrators, and the difference in the quote
 Plant aisle
Steel and code are quoted by different people
The building panel fabricators make the enclosure and wire it to a drawing. An integrator writes the logic and commissions the line.
On a retrofit, ask which of the two signs the test sheet.
Most quotes mix the two into one figure. Split them into steel, copper, drive and software, and the comparison becomes possible.
When the work touches industrial automation and control systems, the integrator owns the sequence and the fabricator owns the cabinet. Both can be right and still leave a gap at the terminals.
A control panel company that does both should say so in writing. Name the people who will be on site.
A shop working to ISO 9001 hands over the routine test record without being asked. That record is what your insurer will want after a fault.
Where a retrofit blocks the aisle
Adding a section to an existing row is the cheapest scope, and the one that fails inspection most often.
Keep 800 mm of clear working space in front of the doors. Where the panel is deep, keep 1000 mm. Measure the door swing as well as the footprint.
A retrofit that ends up blocking electrical panels along a walkway breaks the escape route. It also breaks the clearance rule. Move the row, not the rule.
Pump rooms are the usual victim. An alternating sump pump controller added to a wet well room often lands in the only free metre. That metre was the walkway.
Frequently asked questions
How long does a VFD panel retrofit take?
Can a drive go into the existing enclosure?
Do old motors need a reactor or a filter?
Is a retrofit cheaper than a new panel?
Can I keep the existing starters and add a drive?
What should the survey report contain?
Who owns the drawing after the retrofit?
Final thoughts
Pick the company by the survey it produces, not by the panel it shows. The report tells you whether the vendor has stood in front of an old machine before.
Send us the motor list and the cabinet photos. We will return the scope per motor, the enclosure check and a price for each of the three scopes.
Send the motor list first
Give us the nameplate data, the cable lengths and one photo per cabinet. We will return the survey sheet, the enclosure check and a scope for each motor.
Contact Giantele